How to glue acrylic together is usually answered with a cement name, and the answer is incomplete. A retail fit-out in Rotterdam sent back nine acrylic display cases last spring, all cracked within six weeks along the same corner. Nothing had been dropped and the joints looked clean at handover. The cases had been bonded with a fast capillary cement, clamped for forty minutes and packed the same afternoon. The joint had cured; the panel had not relaxed.
Bonding acrylic is a controlled chemical joint, not a glue-and-hold operation. The cement dissolves a thin layer of the two faces and lets the polymer chains re-form across the gap, so the strength of the joint is decided before the clamp comes off. Get the gap, the cement and the cure period wrong and the assembly fails in the field rather than on the bench.
Joint preparation when you glue acrylic together
Capillary cement, usually a low-viscosity dichloromethane blend, works only on joints that close to within 0.1 to 0.2 mm. It flows in by surface tension, cures in minutes and gives a nearly invisible line. It is the right choice for a square, machined edge on cast sheet. It is the wrong choice for a flame-polished edge, a sawn edge or a joint with a visible gap, because it cannot fill volume and leaves a line of air behind the face.
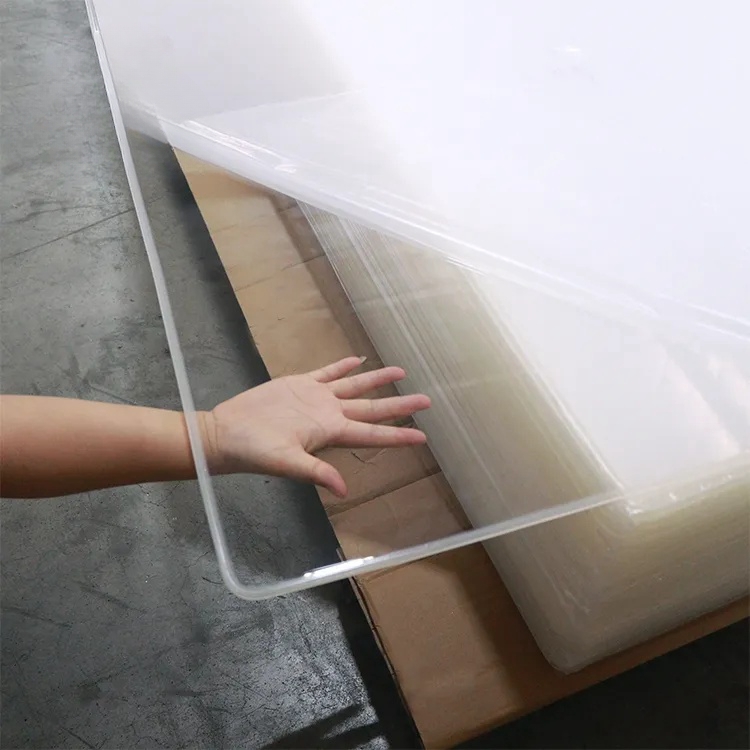
Gap-filling cement, a thixotropic two-part acrylic or a viscous solvent type, fills 0.5 to 1.5 mm and holds the joint while it cures. On 15 mm and thicker sheet the extra volume is what prevents a star crack at the corner, because the load is spread along the bond rather than concentrated at the edge. Buyers who specify one cement for every joint usually end up with capillaries on thick corners.
Preparation decides the result before the cement does
Both faces must be machined square, then wiped with a clean lint-free cloth and allowed to dry. Solvent wiping with an alcohol before bonding sounds thorough and is actually harmful: it leaves a residue that blocks the cement from wetting the surface. Keep the protective film on the face that will be visible, and remove it only after the joint has cured.
Clamping pressure should be even and light. A joint clamped hard squeezes the cement out of the line and leaves a dry joint that reads perfectly and fails in tension. Masking tape on the outside faces at 150 mm intervals, plus a flat caul, is enough for most assemblies up to 20 mm.
Cure, then relieve
A capillary joint reaches handling strength in about 30 minutes and full strength in 24 hours. A gap-filling joint needs 24 to 48 hours before any handling load. Cutting a joint flush, drilling it or routing it before that window opens introduces stress at exactly the point the cement is still shrinking, which is the source of the crack pattern that appears two months later.
Annealing is the step that most workshops skip. A bonded assembly that will live outdoors, or that will be cleaned daily, benefits from a 2 to 4 hour soak at 70 to 80 °C followed by a controlled ramp down of no more than 10 °C per hour. That relieves the stress the cement introduced and keeps the joint clear rather than crazed.
If the assembly involves cutting and drilling after bonding, the sequence in the fabrication walkthrough on cutting, drilling and polishing acrylic sheet is worth reading before the cement is ordered, because the order of operations decides whether the joint survives the machining.
The four failures worth recognising
A white line along the joint means the cement dissolved too much material and the joint is now a weak, porous seam. A star crack at a corner means point load during cure. A joint that separates cleanly after a week means the surface was contaminated before bonding. A joint that crazes after two summers means the assembly was never annealed. Each has a different fix, and only the first is a cement problem.
Send your assembly drawing with the sheet thickness, joint type and annual quantity to oversales@rpplexiglass.com, and we will quote cast sheet with a bonding trial panel so the joint can be approved before the first production lot.
Frequently Asked Questions
Can I glue acrylic with cyanoacrylate or epoxy?
Cyanoacrylate is not suitable: it cures brittle, bonds poorly to PMMA and leaves a visible white line under load. Standard epoxy adheres but the joint stays visible, and a rigid epoxy at a moving joint cracks the sheet rather than the bond. Solvent cement is the only method that produces a joint close to the parent material in strength and appearance.
How long before I can handle a bonded acrylic assembly?
Plan on 24 hours minimum for a capillary joint and 48 hours for a gap-filling joint before any handling load, and 72 hours before machining the joint. In cold weather below 15 °C, double the window or move the assembly into a warm room, because cure rate falls sharply and a cold joint is a weak joint.
Does the joint stay clear on 20 mm cast sheet?
It can, provided the edges are machined square, the cement is the gap-filling type and the assembly is annealed after cure. On thick sheet the joint line is wider, so any contamination or trapped air is more visible. Ask for a sample joint in the same thickness before approving a production run.